O-Ring Groove Design Guide | ISO 3601-2:2025
An O-ring may have the right material and dimensions and still leak after installation. In some cases, the problem lies in the groove rather than the seal itself. Sometimes, it is the groove that is the source of the issue, whereas, the seal itself is in order. Groove depth, width, dimensional tolerances and hardware clearance are all parameters that affect an O-ring's behavior under pressure.
ISO 3601-2:2025 standard is about the sizing requirements for the groove for hydraulic and pneumatic O-rings in general. This norm can be used in conjunction with or without back-up rings. This document outlines the sizes that are useful and gives them in numbers but it must be understood that the housing is only part of the design of the final product and it has to be modified according to the working conditions.
A groove drawing can appear quite simple on page. Still, real life experience has revealed that even a minute variation in dimension can have a significant impact on the seal's compression. In this article you will find examples explaining the importance of these variations which need to be taken care of before production commences.
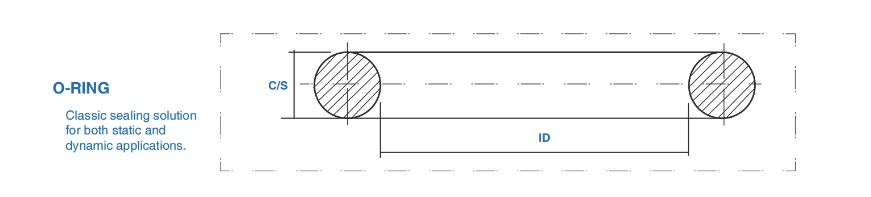
1. O-ring Squeeze: why groove depth is important
The O-ring squeeze is the decrease in seal cross-sectional height after installing.
It allows rubber to put pressure upon itself and also the opposite metal surface.
An inadequate amount of squeeze may lead to not enough sealing surface.
On the other hand, an excessive squeeze causes seal to become very deformed and worn out, especially in areas where seal movement is occurring.
Take a simple axial face seal setup:
Squeeze (%) = [(O-ring cross-section − Gland depth) / O-ring cross-section] × 100
A math operation is easy enough. What's harder is finding the right groove depth since all factors like working pressure, tolerances, material behavior and especially temperature have to be considered.
Design Example: A Small Change in Groove Depth
Consider a hypothetical static axial face-seal application using an O-ring with a nominal cross-sectional diameter of 3.00 mm.
Two installed groove depths are being compared: 2.70 mm and 2.40 mm. Their calculated nominal squeeze values are 10% and 20%, respectively.
Design Parameter | Design A | Design B |
O-ring cross-section | 3.00 mm | 3.00 mm |
Installed groove depth | 2.70 mm | 2.40 mm |
Nominal squeeze | 10% | 20% |
In Design A, the O-ring is compressed by 0.30 mm. In Design B, the compression increases to 0.60 mm.
Although the groove depths differ by only 0.30 mm, the nominal squeeze doubles.
This difference can have a meaningful effect on initial sealing contact. If squeeze is insufficient for the application, reducing groove depth may be one possible design adjustment.
However, Design B is not automatically the better option.
Higher squeeze also changes the available space in the groove and the stress imposed on the seal. Before either design is approved, the engineer must review gland fill, operating conditions, installation geometry and the dimensional limits of both the O-ring and the hardware.
This is a hypothetical calculation example, not a documented customer case or a universal design recommendation.
Manufacturing Tolerances Can Change the Result
Nominal dimensions do not tell the whole story.
Consider another illustrative arrangement with a 2.62 mm nominal O-ring cross-section and a 2.10 mm nominal gland depth. Assume the cross-section tolerance is ±0.08 mm and the depth tolerance is ±0.05 mm.
Condition | Cross-Section | Gland Depth | Squeeze |
Minimum | 2.54 mm | 2.15 mm | 15.4% |
Nominal | 2.62 mm | 2.10 mm | 19.8% |
Maximum | 2.70 mm | 2.05 mm | 24.1% |
These assumed tolerances produce a squeeze range from approximately 15.4% to 24.1%.
This is why a drawing that appears acceptable at nominal dimensions may still require further evaluation at its dimensional extremes.
The figures illustrate tolerance effects. They are not recommended squeeze limits for every sealing application.
2. Gland Fill: Leaving Enough Room for the Rubber
Rubber behaves differently from a compressible foam. Under typical sealing conditions, its volume changes very little when compressed. Instead, the O-ring changes shape and occupies the available groove space differently.
Gland fill describes how much of that space is occupied by the seal.
A groove with insufficient free volume can create problems when the rubber expands due to heat or absorbs fluid from its operating environment.
Depending on the material and conditions, swelling may further increase the occupied volume.
For example, a groove that accommodates an O-ring at room temperature may offer less free space after the material has been exposed to elevated temperatures or a swelling medium.
This matters when replacing an existing O-ring with a different rubber compound. Even if the nominal dimensions are identical, the materials may behave differently in service.
Gland fill should therefore be checked using the selected material's properties, the groove dimensions and the expected operating environment.
3. Installation Stretch and O-Ring Dimensions
An O-ring is often stretched slightly when installed over a piston or into a groove.
A certain amount of stretch may help hold it in position. But stretching also affects the cross-sectional dimensions of the rubber.
For a simple circular installation, the approximate stretch is calculated as:
Stretch (%) = [(Installed diameter − Free O-ring ID) / Free O-ring ID] × 100
Excessive stretch can reduce the effective cross-section, which may change the installed squeeze.
This means that selecting an O-ring by inner diameter alone can be misleading.
The installation diameter, original cross-section and resulting deformation all need to be considered together.
Installation damage is another possibility worth checking. An O-ring may be cut while being pulled over a threaded section, or twisted as it is pushed into a narrow groove. Such damage might not be obvious once the assembly is complete.
A suitable lead-in chamfer, clean mating parts and an installation method appropriate for the material can make a difference. Lubrication, where permitted, must also be compatible with the elastomer and working fluid.
4. Pressure and Extrusion: Look at the Clearance Gap
An O-ring can be damaged even when its groove dimensions look correct on the drawing. One thing worth checking is the gap between the mating components.
Under pressure, the rubber tends to move toward this gap. If the opening is too large for the pressure and material, part of the O-ring may be forced into it. The damage is not always immediate. After repeated pressure cycles, the seal may develop small tears or an irregular edge.
The gap in an assembled machine may also differ from the measured gap on an unloaded part. Metal components can deflect under pressure, so the clearance needs to be assessed under the expected operating conditions.
Rubber hardness is one factor in extrusion resistance, but it is not the only one. A harder compound may help in some applications; it will not necessarily solve a problem caused by excessive clearance. Pressure, temperature and the properties of the selected material all matter.
A back-up ring can provide support beside the O-ring and limit the space into which the rubber can move. PTFE is one material used for back-up rings, although the appropriate design depends on the application. If pressure can act from either direction, support on both sides may be necessary.
There is also a space requirement to consider. A back-up ring occupies part of the housing, so the groove design must accommodate it.
When an O-ring shows signs of extrusion, check the damaged seal alongside the hardware. The clearance gap, working pressure and direction of pressure are useful starting points before deciding whether the material, groove or back-up arrangement needs to change.
5. Surface Finish: A Detail That Is Easy to Overlook
A groove can meet its drawing dimensions and still damage an O-ring. A burr left after machining, for example, may cut the rubber as the seal is pushed into place. The mark can be small enough to miss during assembly, yet still affect sealing performance later.
Pay particular attention to the route the O-ring takes during installation. Threads, sharp corners and rough edges can all damage the seal before the equipment is put into service. Checking the groove alone may not be enough; the mating parts should be inspected too.
Movement changes the situation. In a static joint, the O-ring stays in place once assembled. In a dynamic application, it slides against another surface, making friction, lubrication and wear more important. Surface finish requirements therefore depend on how the seal is used and where the sealing contact occurs.
A shiny surface is not proof that it is suitable for an O-ring. The groove wall and the surface that contacts the seal may have different requirements, depending on the design.
This is worth remembering when replacing a leaking seal. It is easy to suspect the rubber compound or the O-ring size first, but the hardware may be part of the problem. A damaged groove edge, misalignment or marks from previous assembly work can also affect the seal.
The removed O-ring may help explain what happened. A cut, a flattened section or uneven wear gives the engineer something to investigate, but none of these signs proves the cause on its own. Compare the seal with the groove and consider the service history before deciding what to change.
6. What Buyers Should Check Before Placing an Order
For replacement O-rings, customers sometimes have only an old seal and a few measurements. That may be enough to begin a discussion, but it is not always enough to confirm the correct specification.
A drawing of the groove is particularly helpful. It shows the space available for the seal and allows the supplier to consider the installed dimensions instead of relying solely on the O-ring's free dimensions.
For a custom project, the following information can help clarify the requirements:
Information | Purpose |
O-ring ID and cross-section | Confirm seal dimensions |
Groove drawing | Review housing geometry and tolerances |
Rubber material and hardness | Assess material suitability |
Operating temperature | Evaluate thermal requirements |
Working fluid | Check chemical compatibility |
Maximum pressure | Evaluate potential extrusion concerns |
Static or dynamic operation | Identify relevant design considerations |
Estimated order quantity | Assess manufacturing options |
Not every customer will have all these details at the inquiry stage.
For example, someone replacing a failed seal may know the equipment model and working fluid but not the original rubber compound. In that situation, photographs, housing measurements and information about how the seal failed may help narrow down the possible causes.
A damaged O-ring can provide clues. A cut along one edge suggests a different problem from rubber that has been forced into a clearance gap. However, neither observation should be treated as a confirmed diagnosis without checking the hardware and operating conditions.
The aim is to understand what the seal must do before deciding what to manufacture.
7. Custom O-Rings: What Yida Can Review
A custom O-ring inquiry usually starts with a size, a drawing or a sample. But if the seal needs to fit existing equipment, the groove dimensions can be just as important as the O-ring itself.
At Dalian Yida Precision Rubber Products Co., Ltd., our work covers rubber material development, mold making, molding and product testing. These capabilities support both standard O-ring orders and projects that require customized dimensions or materials.
For an existing assembly, the first thing to clarify is often the space available for the seal. A groove drawing helps show whether the proposed O-ring dimensions are suitable. If the application involves a different fluid or a wider temperature range, the rubber compound also needs to be reviewed rather than selected by size alone.
Timing matters on new projects. If a groove needs to change, finding that out before the tooling and metal parts are completed can avoid extra work later. The information available varies from project to project, so drawings, material requirements and operating conditions are useful starting points.
Yida manufactures standard and custom rubber O-rings for industrial applications. You can view our O-ring products or share your requirements for a project-specific discussion.
8. Before Finalizing the Groove Drawing
With a 3.00 mm cross-section, changing the installed groove depth from 2.70 mm to 2.40 mm changes the calculated squeeze from 10% to 20%. A separate tolerance example shows how manufacturing variation can affect compression even when the nominal dimensions remain unchanged.
These calculations answer only part of the design question.
A groove also needs sufficient room for the rubber, an appropriate clearance gap and surfaces that will not damage the seal during installation. The selected elastomer must remain suitable for the working fluid and operating temperature.
ISO 3601-2:2025 is a reference for housing dimensions in general hydraulic and pneumatic applications. It does not remove the need to evaluate the actual conditions in which the O-ring will operate.
For custom O-ring projects, customers are welcome to share their drawings, material requirements and available operating information with Yida.
If some details are still uncertain, those questions can be identified during the initial technical discussion rather than left until after production.